sales@sztimeast.com
+86 159 8954 1416
A rotary ultrasonic welding system should be specified around the production result you need: acceptable assemblies
delivered at the required rate, with a workable loading method and a clearly defined inspection process.
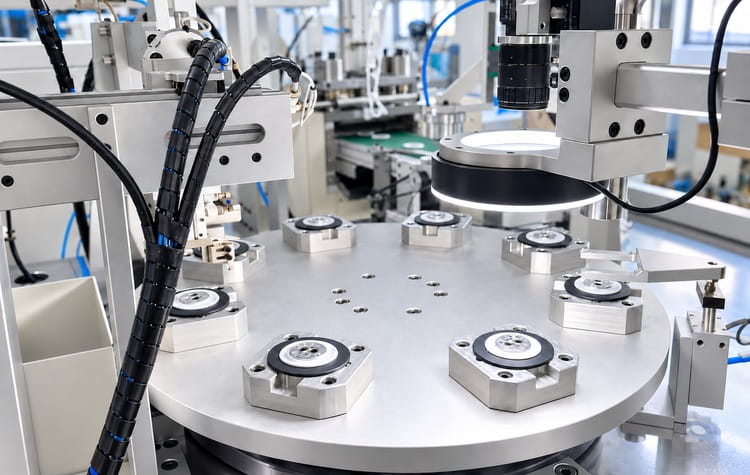
Start with the product and production requirements before deciding how many table positions or welding heads to install.
If you are still comparing equipment layouts, first read how rotary ultrasonic welding machines work and when to use them.
State the number of acceptable assemblies required per hour or shift, together with the available production time.
Include planned breaks, staffing, product variants and expected changeovers. Distinguish the machine’s theoretical
cycle rate from the number of acceptable parts it must deliver during normal operation.
For initial planning:
Theoretical output per hour = 3,600 ÷ index-cycle time in seconds × completed assemblies per index
For example, a four-second index cycle delivering one completed assembly per index gives a theoretical rate
of 900 assemblies per hour.
This is an illustrative calculation, not a TIMEAST equipment specification. Actual acceptable output will
be lower when stops, speed losses and rejects are included.
Ask the supplier to define the conditions behind any quoted output figure.
Ultrasonic vibration time is only one part of the welding station’s sequence. The station may also require clamping,
horn approach, hold time and retraction.
For a simple synchronized table, with operations running in parallel during each stop:
Index-cycle time ≈ longest station sequence + table indexing and settling time
Additional time may be required when stations share equipment or operations must occur sequentially.
Build a timing chart covering:
| Operation | What to include |
| Loading | Part pickup, orientation, insertion and confirmation |
| Welding | Clamping, approach, welding, hold and retraction |
| Inspection | Part positioning, measurement and result processing |
| Unloading | Gripping, removal, sorting and placement |
| Indexing | Clearance confirmation, table movement and settling |
If manual loading takes longer than the welding sequence, faster welding alone
will not increase the machine’s output.
More table positions do not automatically mean more finished parts.
Table positions provide locations for process steps. Welding heads provide access to the joints
that must be welded. A machine can therefore have several table positions but only one welding head.
An illustrative sequence might include:
Load the first component.
Add the second component and check orientation.
Weld the assembly.
Perform a required inspection.
Unload and separate parts by result.
Confirm that the fixture is empty.
Some applications can combine these steps; others need additional positions or equipment outside the table.
Also confirm the number of assemblies completed per index. Six fixtures moving around a table
do not necessarily deliver six finished assemblies on every index.
Provide actual samples, material grades, joint drawings and measurable quality requirements.
The generator, actuator, horn and fixture should be selected as a coordinated welding package.
Generator wattage alone does not establish whether a system suits the application.
Discuss:
Required joint strength, sealing performance and appearance.
Access to each welding location.
Component tolerances and fixture support.
Proposed weld control mode.
Parameters available for monitoring and recording.
A PLC coordinates machine operations, but the selected ultrasonic equipment determines
which welding functions and process measurements are available.
For applications that still need process evaluation, start with ultrasonic welding sample testing
Evaluate handling against the actual part geometry, surface finish and product mix.
| Production condition | Question to resolve |
| Cosmetic surfaces | Can the feeding and gripping method avoid unacceptable marks? |
| Similar-looking orientations | How will incorrect placement be detected? |
| Flexible or easily tangled parts | Can components be presented consistently? |
| Multiple variants | Which fixtures, guides and grippers must change? |
| Sustained production | How will materials be replenished and finished parts collected? |
Manual loading may remain practical even when welding and unloading are automatic.
Compare the complete staffing requirement, including replenishment and fault recovery, rather than
assuming that an automatic unloading unit makes the entire process unattended.
Choose the inspection method according to the defect that must be detected.
Presence sensors can check missing components. Vision systems may assess visible features.
Sealing requirements may call for a suitable leak test. Joint strength requires an appropriate validation
and testing plan.
Weld-process monitoring can identify cycles outside agreed limits, but a process pass signal alone
does not prove every required product property. Specify how the system will:
Associate inspection results with the correct fixture or assembly.
Separate failed and untested parts.
Confirm successful removal.
Respond to a full reject container.
Handle assemblies affected by an interrupted cycle.
These details prevent uncertain parts from re-entering normal production without review.
When connecting the rotary machine to other equipment, define the signals and operating
responsibilities before construction.Typical topics include:
Upstream part availability.
Downstream readiness and blocked conditions.
Machine ready, running, complete and fault signals.
Product recipe selection.
Required production and quality data.
Recovery after jams, interrupted welds or power loss.
Confirm the communication method and which supplier is responsible for each interface.
Safeguarding and safety control functions must also be considered as part of the integrated
equipment design. Normal production signals do not replace those functions.
Ask what must change when switching products: fixtures, horns, feeder guides, grippers,
inspection settings and recipes may all be involved.
Define changeover time against an agreed scope, including first-piece verification.
Also review access for cleaning, fixture checks, horn replacement and servicing.
Confirm the factory’s available space, utilities and material flow.
These details affect how reliably the equipment can deliver its planned output over time.
A quotation should describe how the proposed performance will be verified.
| Acceptance item | What to agree |
| Weld quality | Test methods and acceptance limits |
| Output | Acceptable assemblies produced over a defined run |
| Operating conditions | Staffing, material supply and included inspection steps |
| Reliability | Run duration and treatment of stops and resets |
| Detection and sorting | Challenge tests using agreed defective or incorrect samples |
| Changeover | Included tasks and first-piece approval |
| Handover | Documentation, training and backup requirements |
Use representative production components during acceptance testing. Record any differences
between the test arrangement and the intended factory installation.
A short demonstration of successful welds should not be treated as proof of sustained production capacity.
For a useful configuration review, send TIMEAST:
Part drawings or clear photos and material grades.
Welding locations and quality requirements.
Required acceptable output per hour or shift.
Product variants and changeover frequency.
Preferred loading method and available operators.
Inspection and sorting requirements.
Available space and connections to other equipment.
These inputs help define the station sequence, welding package and handling arrangement
before a detailed quotation is prepared.
View the custom rotary indexing ultrasonic welding system as a starting point for discussing your project.
Phone: +86 159 8954 1416
E-mail: sales@sztimeast.com
Whatsapp:+86 159 8954 1416
Add: Building 5, Huixin Intelligent Industrial Park,Guangming, Shenzhen,China 518107